

Engineering Resources · Operating Parameters
Engineering fundamentals
The Operating Parameters That Decide Filter Press Performance
A filter press spec sheet is a story about pressure, time and dryness — and the numbers only make sense when they are measured against the same conditions. This page sets out the parameters operators set on a daily basis, the ones a proposal should put in writing, and the ones a bench test confirms on your sludge.
Why parameters matter
Four Numbers That Decide Whether the Machine Will Do the Job
A filter press is a mechanical press for liquids. The output — cake dryness, throughput, running cost — is a consequence of how pressure, time and conditioning are set. Read the spec sheet and the trial report through these four lenses and the rest of the comparison becomes a lot easier.
Filtration pressure
Feed and squeeze pressure set how the cake is built and how dry it gets. Typical chamber presses run 0.6–0.8 MPa feed; membrane presses add 1.5–2.0 MPa squeeze. Above that, returns diminish and cloth life shortens.
Cycle time
From feed start to cake drop. Typical 20–60 minutes per cycle on chamber presses, depending on cake thickness, feed solids and the dryness target. Cycle time is what sets daily throughput for a given filtration area.
Cake dryness
The dry-solids content of the discharged cake — typically 25–35 % on chamber presses and up to ~50 % on membrane presses with air blow. Achievable dryness is a function of sludge, not just machine.
Specific throughput
Kilograms of dry solids per square metre of filter area per hour (kg DS / m²·h). It ties filtration area, cycle time and feed solids into one number — the one to compare across quotes.
A typical cycle
Parameter by Parameter, Phase by Phase
Every cycle is a sequence of phases, and each phase has a setpoint the operator — or the PLC — controls. Skim the diagram and the rest of the spec sheet reads itself.
Feed pump delivers conditioned sludge into the chambers at controlled flow. The parameter is feed rate, capped by the pump and the feed-pressure relief.
Filtrate passes the cloth and the cake builds. The parameter is pressure profile, held to a target until flow drops below the end-of-filtration setpoint.
On membrane presses, water inside the elastomer plate compresses the cake. The parameters are squeeze pressure and hold time, which set the final dryness.
Compressed air pushes residual water out of the cake. The parameter is blow pressure and duration, removing surface moisture without re-wetting the cake.
Plates open, cake drops, the cycle restarts. The parameters are plate-shifter speed and cloth-wash interval — they decide uptime and cloth life on the next cycle.
Numbers like 0.6 MPa or 35 % dryness are typical, not guaranteed — they are confirmed on a bench test on your sludge, and they are the numbers Loway puts in the proposal.
On the control panel
The Setpoints Operators Adjust Every Day
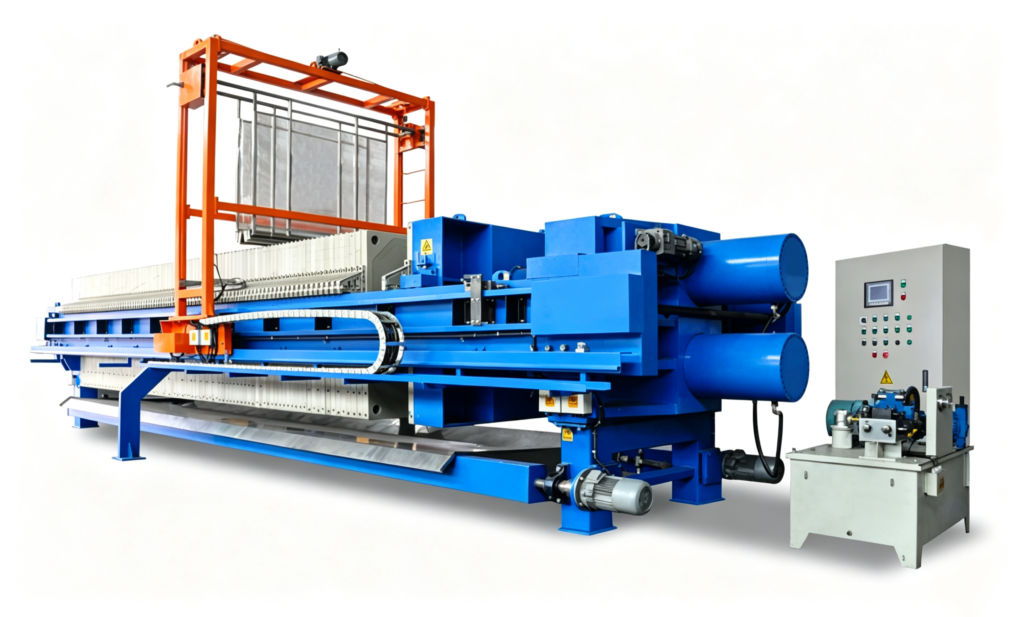
- PAR-3.1Feed pressure setpoint — the maximum pressure the feed pump will deliver before the relief opens, usually set just below the pump’s continuous rating.
- PAR-3.2Squeeze pressure & hold — for membrane presses, the secondary pressure the elastomer reaches and how long it holds before the cycle advances.
- PAR-3.3Air-blow pressure & time — set on the same screen; too low leaves surface moisture, too high lifts fines back into the cloth.
- PAR-3.4End-of-filtration setpoint — a flow threshold (or a pressure-decay time) that ends the feed phase and starts squeeze or air blow.
- PAR-3.5Cloth-wash interval & cycle count — automatic washes after N cycles, with alarm thresholds on differential pressure across the cloth.
- PAR-3.6Alarms & trend logs — over-pressure, low flow, plate-shifter fault and the operating log; the data the maintenance team reviews every week.
Loway’s standard cabinet ships with the parameter set loaded for the machine ordered. The setpoints are yours to change later — we hand over the load sheet and a one-page “what each parameter does” reference. Need a spare or a parameter sheet later? →
On a quote or trial report
The Numbers a Proposal Should Put in Writing
- Filtration area — total active cloth area in m². With cake thickness and feed solids, this sets the cycle time and the daily throughput.
- Chamber volume (or membrane volume) — the wet-cake volume per press, with chamber depth. The volume decides the cake weight per cycle and the discharge rate.
- Max feed & squeeze pressure — the pump and the hydraulic unit ratings. Verify they are continuous ratings, not just peak.
- Cycle time at the agreed dryness target — the number of minutes from “fill” to “cake drop” at a stated dry-solids content. The fairest single number to compare two machines on.
- Conditioning & polymer dose — type, dose and preparation; a polymer number without the conditioning system is a half-truth.
- Power, water, compressed-air duty — the utilities the cycle uses, on a per-tonne basis. Together with the polymer, this is the operating cost you’ll actually pay.
The reliable way to set those numbers is a bench test on a sample of your sludge; a pilot at your site then confirms them at real throughput. See the sizing calculation →
Numbers you can plan on
Set the Targets Before You Buy — We Put Them in the Proposal
Most filter press purchases are decided on three numbers, and most regrets come from setting two of them in a brochure and the third on instinct. Loway’s engineering process fixes all three on the same data before the proposal is written.
Target cake dryness
A single number your downstream handling needs — typically 25–35 % on chamber presses, up to ~50 % on membrane presses with air blow. The bench test sets the realistic value on your sludge.
Target throughput
Tonnes of dry solids per day, at a stated feed-solids range. 1.5–4.5 kg DS / m²·h is a typical envelope — the bench test narrows it to your feed.
Operating cost band
Polymer dose, kWh, water and compressed air per tonne — written to the same target as the dryness and throughput, not optimised independently.
Parameters FAQ
Operating Parameters, Answered
What is a typical filtration pressure for a chamber filter press?
How long is a typical cycle?
Does higher pressure always give drier cake?
Why does the same machine give different dryness on different sludge?
Can I improve dryness on an existing machine without buying new equipment?
How do I compare two filter press quotes fairly?
Do these parameters apply to belt filter presses and screw presses too?
Plan with the numbers
Talk to a Loway Engineer About Your Parameters
Send a sludge sample, share the data you have, or just tell us the dryness and throughput you need. We’ll come back with the parameters your filter press should be sized against, in writing.